

High Temperature Refrigeration Unit
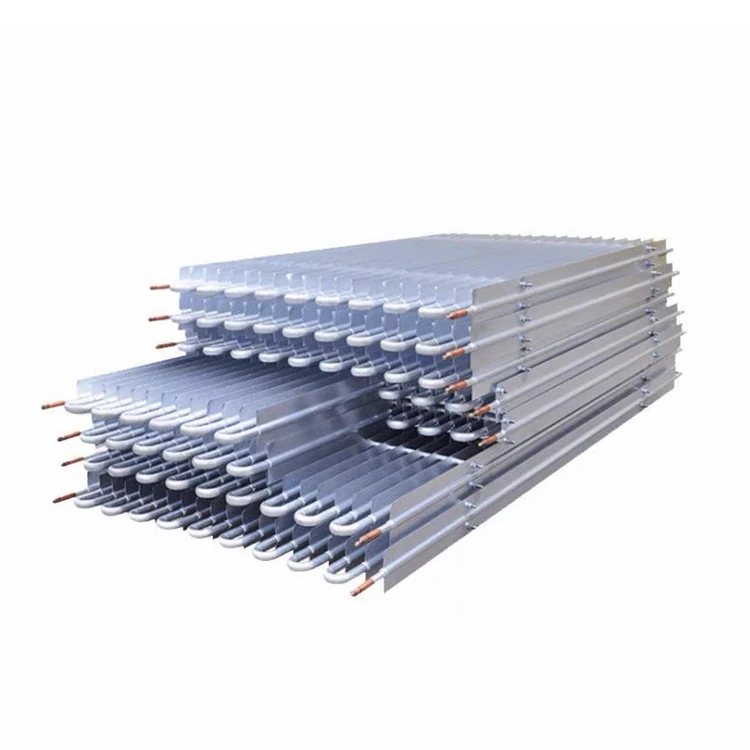
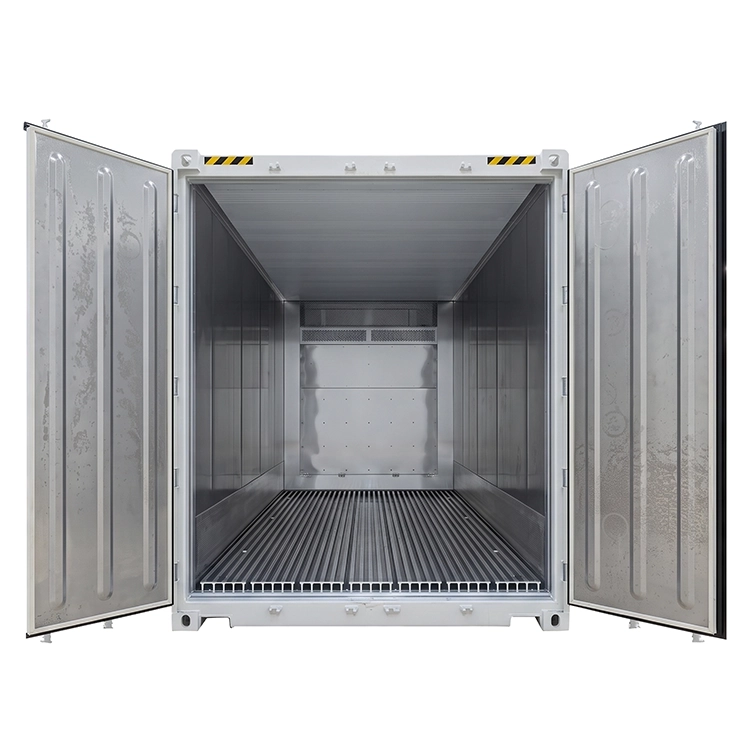
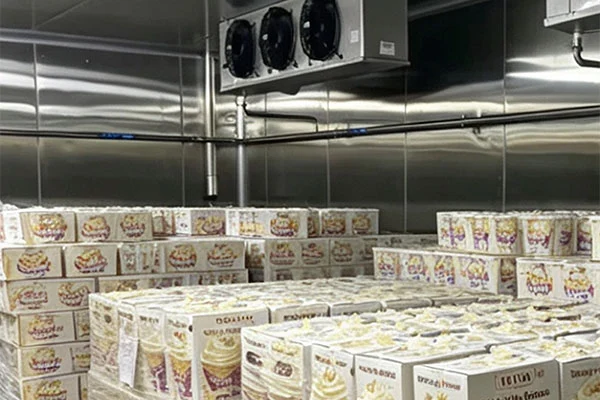
Paulair high temperature refrigeration units are designed for applications such as temperature-controlled warehouses, fresh-keeping storage, food processing facilities, and industrial cooling systems. They are intended for refrigeration applications requiring temperature control above typical low-temperature freezing conditions.
Depending on project requirements, Paulair provides customized high-temperature refrigeration units, equipment configuration, refrigeration system design, and comprehensive technical support based on your exact storage environment, required cooling capacity, and operational conditions.
Applications: Temperature-controlled storage, fresh-keeping rooms, food processing, pharmaceutical warehousing, and industrial cooling.
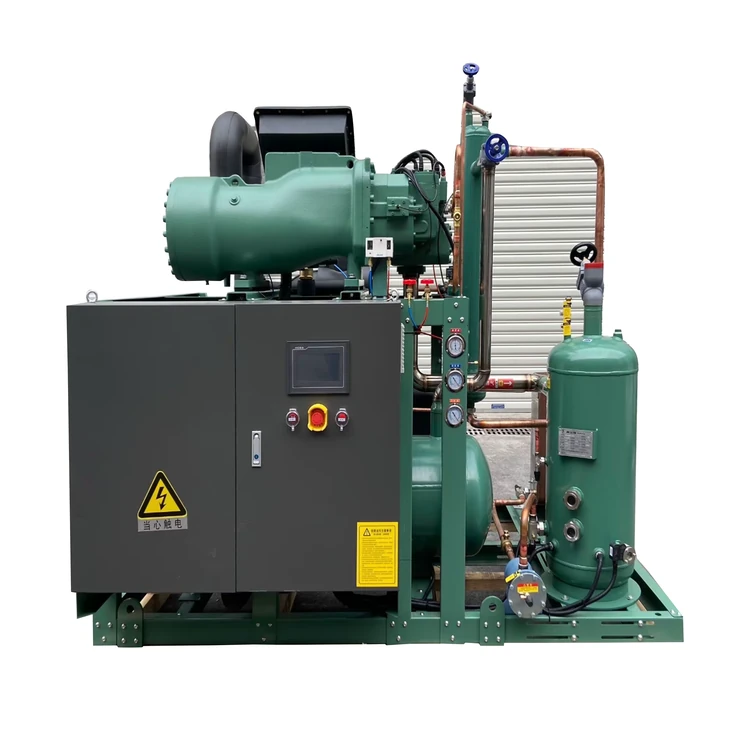
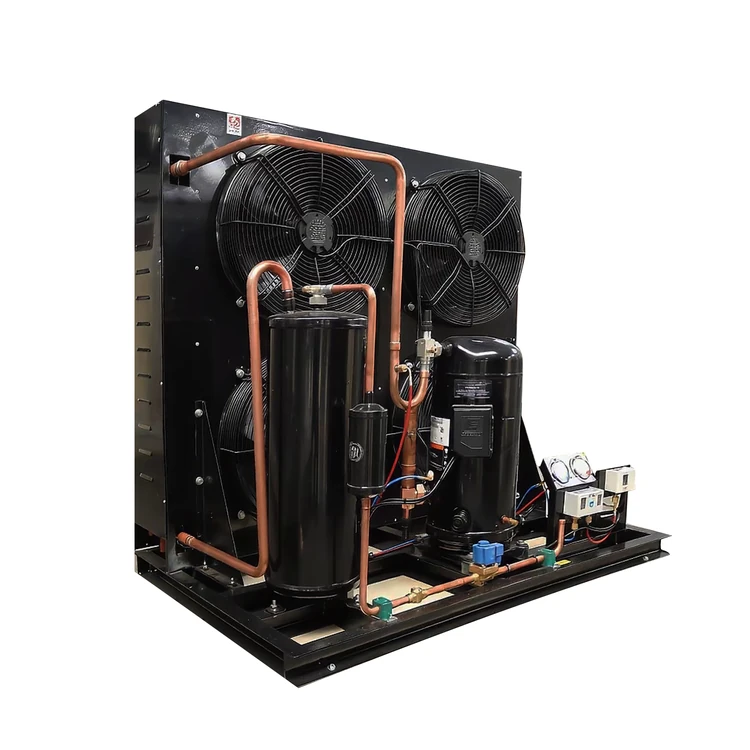
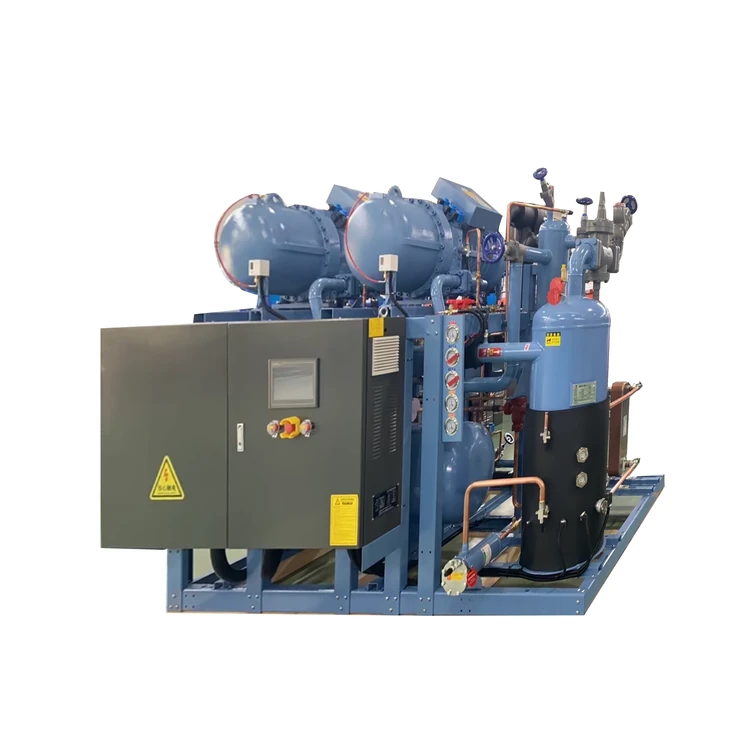
Compressor Options: Scroll, reciprocating, and screw compressors, tailored to your project scale and demands.
Refrigerant Options: Environmentally compliant options including R404A, R507, and R134a, strictly matched to system design and local regulations.
Control Options: Standard manual/digital control, variable-frequency energy-saving control, and optional IoT remote monitoring.
Technical Services: Expert equipment selection, custom system engineering, installation guidance, and 24/7 remote technical support.
Actual cooling capacity, operating parameters, and equipment configuration are engineered according to your specific site conditions to ensure maximum efficiency.


Engineered for Stable Temperature Control Without Deep Freezing
Not every facility requires sub-zero freezing. In fresh-food preservation, pharmaceutical warehousing, and industrial production, maintaining a stable, precise temperature range is critical for protecting product integrity and reducing unnecessary energy waste.
Paulair high temperature refrigeration unit solutions are purpose-built for these applications. By matching high-efficiency compressors, optimized refrigerant circuits, and intelligent controls to your exact operating parameters, we help you eliminate over-engineering and lower operational costs.
Compared to traditional low-temperature freezing systems, our units operate at higher evaporating temperatures. Under comparable design conditions, this yields a significantly lower compression ratio, delivering superior energy efficiency, smoother compressor operation, and extended equipment lifespan.
Every system is custom-configured because actual energy consumption depends heavily on ambient conditions, cooling load, and refrigerant choice. Our engineering team evaluates your exact parameters to ensure optimal matching from day one.
Target Applications and Industry Solutions
Paulair units deliver reliable, continuous cooling across multiple industries where controlled temperatures are vital:
Temperature-Controlled Warehouses
Large storage facilities require robust cooling solutions matched precisely to building envelopes, local ambient conditions, and product turnover. Our systems maintain tight temperature uniformity across every square foot.
Fresh-Keeping Storage
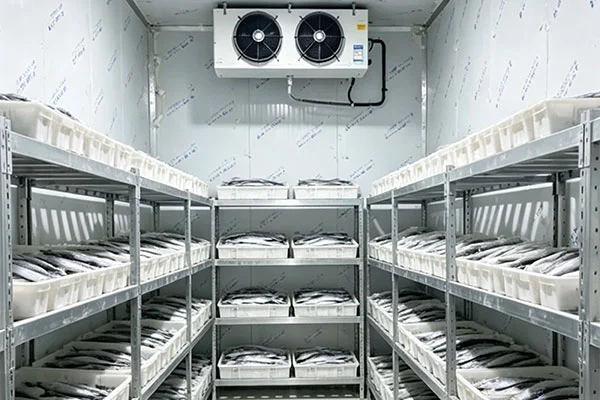
Fresh produce, fruits, and vegetables demand stable environments to prevent spoilage and weight loss. Our precise cooling prevents thermal shock and preserves commercial value.
Pharmaceutical Warehousing
Medical and pharmaceutical goods require strict compliance with storage regulations. Our systems integrate advanced monitoring and automated alarms to provide continuous, auditable temperature security.
Food Processing Facilities
Food processing workshops generate significant internal heat loads from machinery and personnel. Our systems stabilize ambient conditions to meet food safety standards and protect worker comfort.
Industrial Process Cooling
Industrial manufacturing equipment requires continuous heat rejection. Our high temperature refrigeration unit configurations handle heavy industrial duty cycles with minimal downtime.
Core Features, Technology, and System Design
We integrate tier-one components and modular design principles into every high temperature refrigeration unit we build:
- Flexible Compressor Integration: Choose from industry-leading scroll, reciprocating, or screw compressors depending on your cooling capacity requirements.
- Variable-Frequency Energy Saving: Inverter-driven options dynamically adjust compressor speed to match fluctuating thermal loads, preventing short-cycling and cutting power bills.
- Intelligent IoT Remote Monitoring: Monitor real-time temperatures, pressures, compressor status, and receive instant fault alerts directly on your mobile device or control room desktop.
- Global Climate Adaptability: Custom-engineered for overseas environments, factoring in extreme local ambient temperatures, high humidity, and regional electrical supply standards.
Rigorous Manufacturing and Quality Testing Protocols
Before any unit leaves our factory, it undergoes a strict 6-stage quality assurance inspection to guarantee zero-defect startup on your job site:
- Refrigerant System Leak Testing: High-pressure nitrogen testing ensures absolute integrity across all brazed and mechanical joints.
- Pressure Testing: Component vessels and piping are evaluated against strict international safety standards.
- Vacuum Testing: Deep evacuation removes all moisture and air from the circuit prior to initial charging.
- Electrical Safety Testing: Insulation resistance and control logic are fully verified.
- Performance and Run Testing: The high temperature refrigeration unit is test-run under simulated load conditions to verify cooling capacity and COP.
- Complete-Unit Final Inspection: A final physical and operational sign-off is conducted prior to crating and export shipping.
Why Partner With Paulair?
When you choose Paulair, you receive a complete end-to-end partnership designed to protect your investment:
- Direct Manufacturer Value: Premium industrial components without middleman markups.
- Custom Engineering Support: Full thermodynamic load calculations and layout schematics provided before production begins.
- Worry-Free Warranty & Spares: Comprehensive manufacturer warranty backed by readily available replacement parts and lifetime remote engineering assistance.
- Turnkey Guidance: Step-by-step installation manuals, video support, and direct commissioning assistance from seasoned refrigeration engineers.
Frequently Asked Questions
Can a high temperature refrigeration unit be used in a standard cold room?
Yes. It is ideal for fresh-keeping rooms, produce storage, and temperature-controlled warehouses where target temperatures remain above freezing. Applications involving frozen meat or ice storage require low-temperature freezing systems.
What are the efficiency advantages over low-temperature units?
Because they operate at higher evaporating temperatures, these units experience lower compression ratios. This mechanical advantage translates directly into higher energy efficiency and lower long-term power consumption for appropriate temperature ranges.
What information is needed to get an accurate equipment selection?
To design your system precisely, please provide your target storage temperature, room dimensions, insulation thickness, product type, daily loading volume, and local maximum ambient temperature.
Does Paulair provide custom design and after-sales support?
Yes. From initial cooling capacity calculation and custom manufacturing to remote installation guidance and troubleshooting, our engineering team supports your project at every stage.
Get Your Custom Refrigeration Solution Today
Planning a temperature-controlled warehouse, fresh-keeping facility, or industrial cooling project? Let Paulair help you engineer the optimal high temperature refrigeration unit for your facility. Contact our engineering team today with your project specifications for a prompt technical proposal and competitive quotation.
Send Inquiry
Contact Info
-
Address
Xinyuan Avenue, Sangzidian Subdistrict, Tianqiao Borough, Jinan City, Shandong Province, China
-
Tel
-
Submit your project specifications to receive tailored guidance, technical drawings, and cheap factory-direct wholesale pricing from our engineering team today.



News Recommendations