

Container Blast Freezer Room for Pre-cooked Food
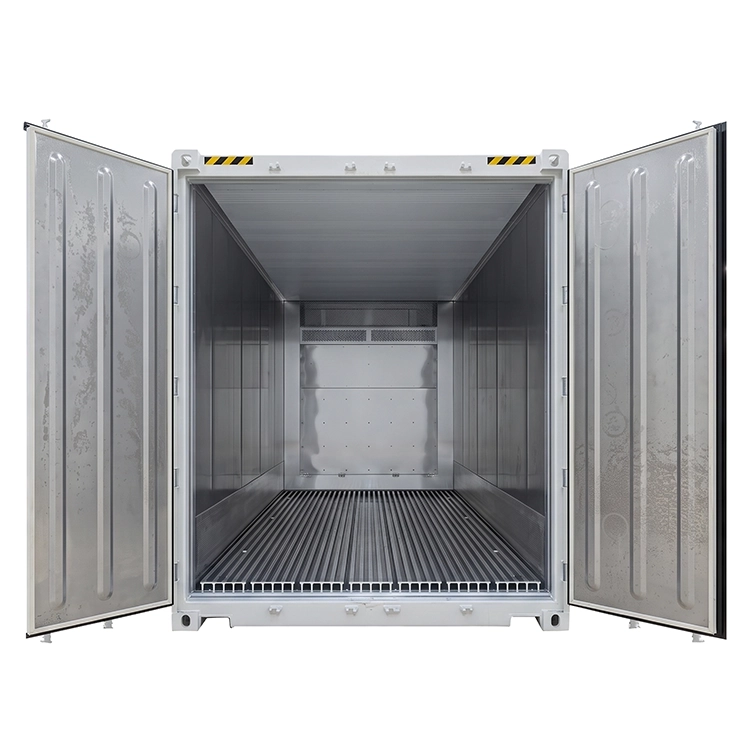
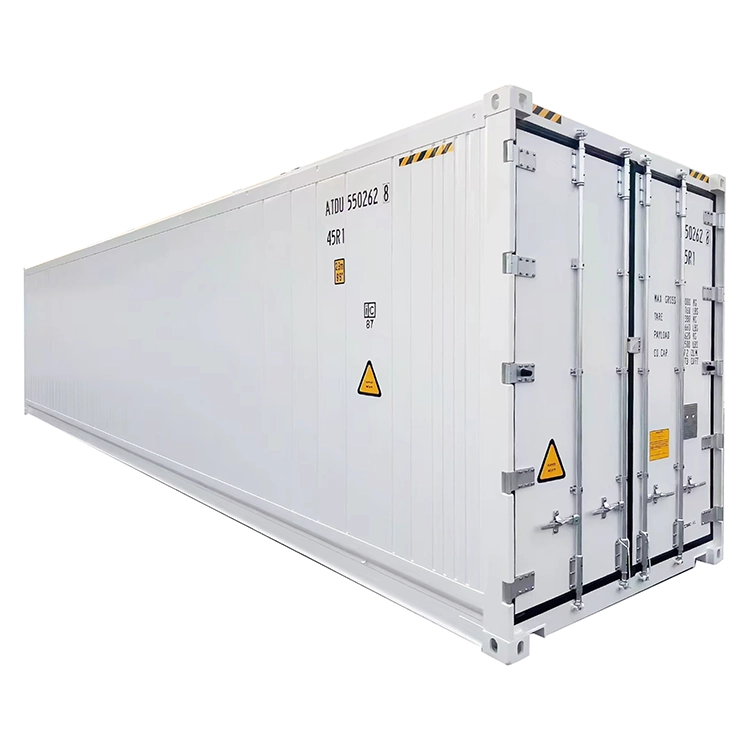
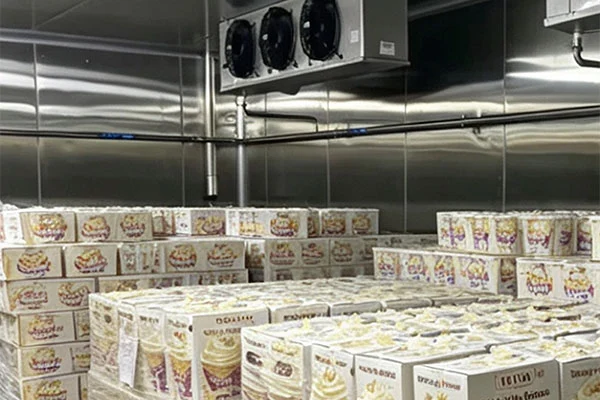
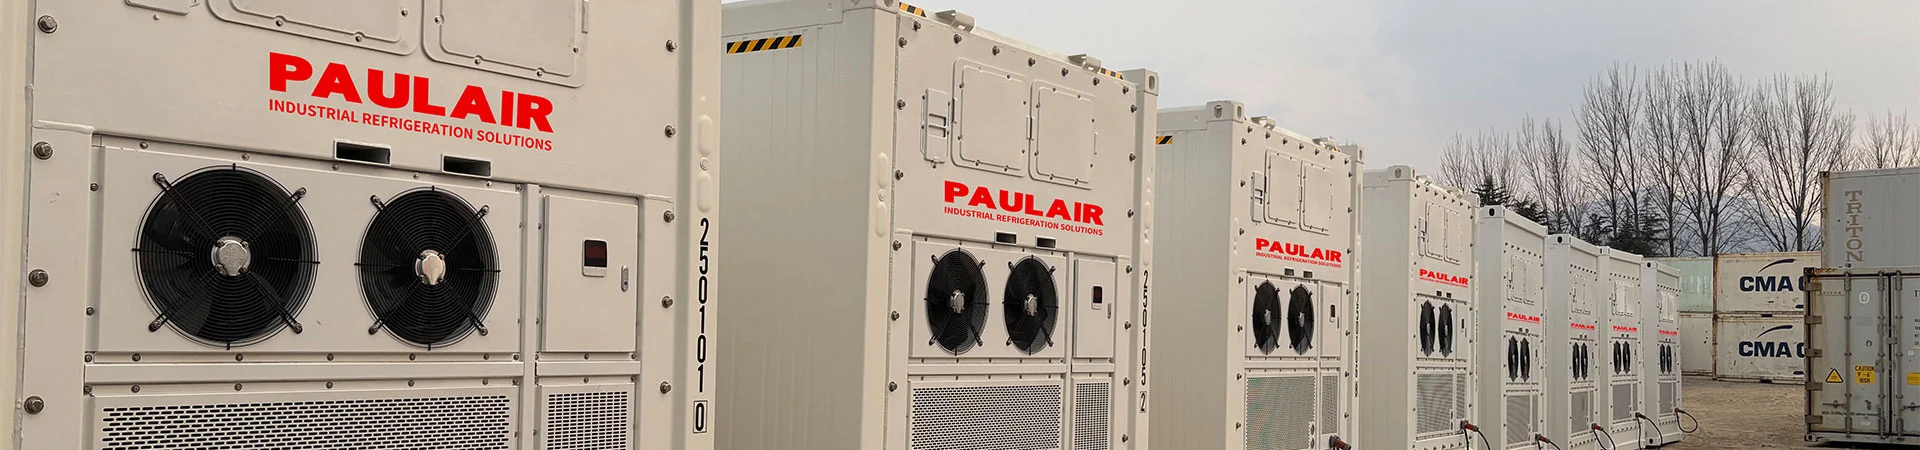
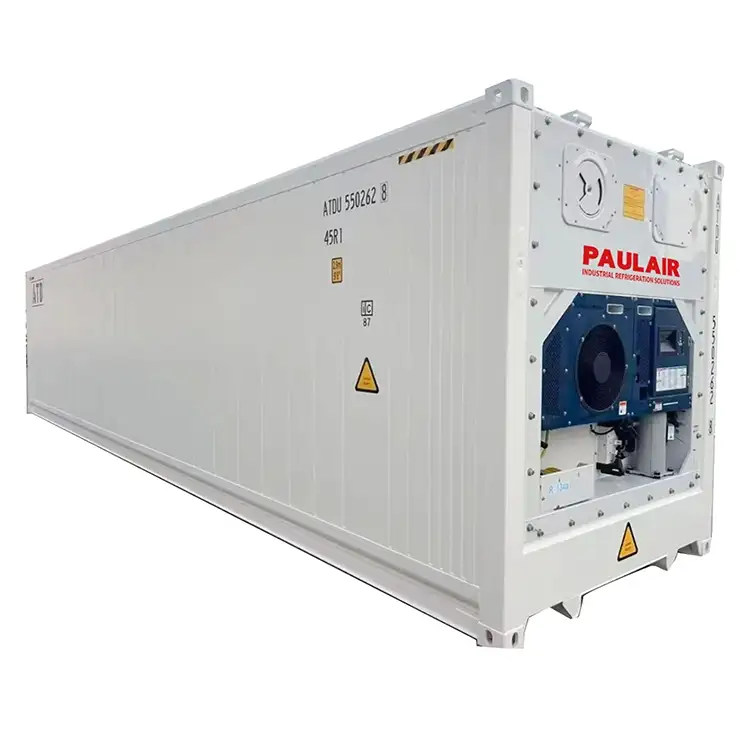
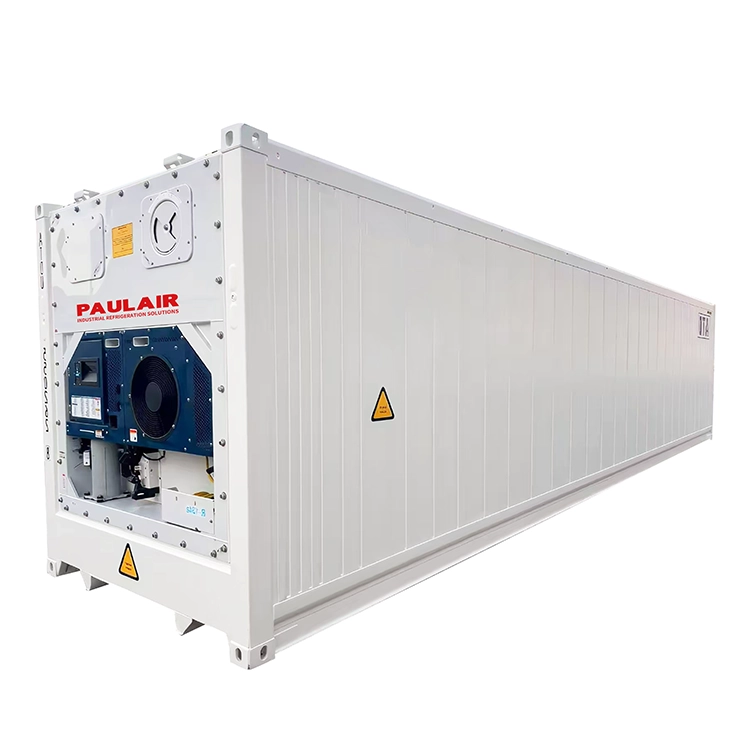
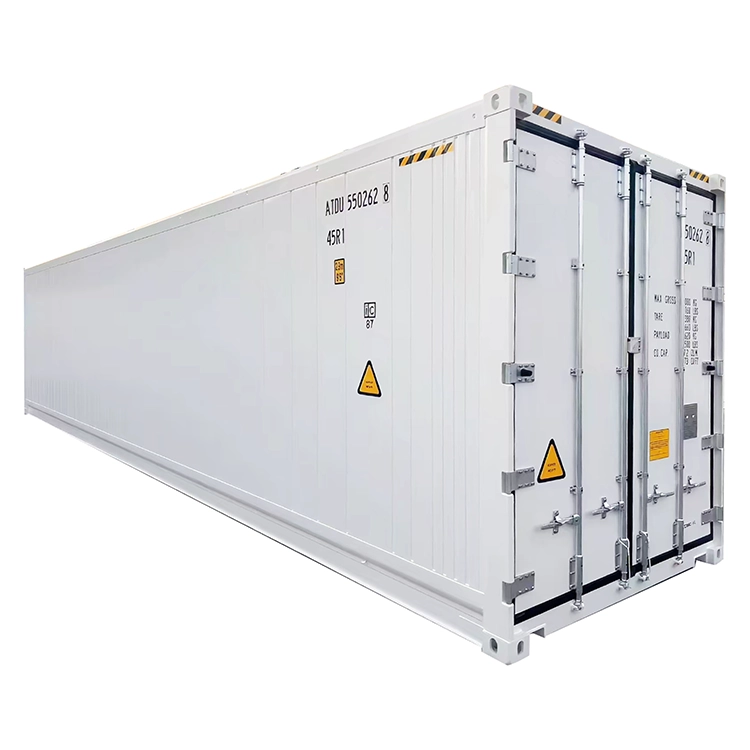
The Container Blast Freezer Room for Pre-cooked Food is suitable for the storage and transportation of frozen prepared dishes such as preserved vegetable braised pork, sour cabbage fish, and Buddha Jumps Over the Wall. It supports operation at -18°C or lower, with a temperature fluctuation target of ±1°C. Designed for multi-component goods including sauces, meats, and vegetables, the unit optimizes odor prevention, cushioning support, and airflow channels based on packaging and stacking methods. It features ≥100mm PU insulation panels, double-sealed doors, and PLC control, with optional IoT monitoring and full-process temperature logging. Available in 20ft, 40ft, and custom non-standard sizes.
Preserving the rich flavors, textures, and food safety of pre-cooked dishes—such as preserved vegetable braised pork, sour cabbage fish, and Buddha Jumps Over the Wall—requires more than just maintaining a standard -18°C. Long-distance transit and storage expose multi-component packaged meals to severe challenges, including cross-contamination of rich spices, surface moisture loss, condensation, and temperature spikes during loading and unloading. To eliminate these risks, our engineered Container Blast Freezer Room for Pre-cooked Food focuses on stringent temperature stability, airtight container sealing, optimized internal airflow, and robust cargo protection rather than relying on generic refrigeration capacity.

Precision Temperature Control for Ready-to-Eat Meals
Our Container Blast Freezer Room for Pre-cooked Food operates consistently at -18℃ or lower, maintaining an exceptional temperature control accuracy of ±1℃. Pre-cooling the container interior before loading actively prevents thermal shock and protects already blast-frozen meals from structural thawing. Designed specifically for cold chain integrity, transportation, and holding, this unit ensures your culinary products arrive at their destination with absolute consistency.

Advanced Odor Prevention and Zoning Architecture
Pre-prepared dishes combine complex sauces, heavy spices, and aromatic ingredients. If package seals fail under transit stress, odor diffusion and flavor contamination can compromise entire shipments. To guarantee product integrity, our units feature customizable internal partitions, buffer supports, and specialized zoning structures. Combined with hermetic container seals that drastically limit external air exchange, your shipments remain completely uncontaminated.

Combating Surface Dehydration and Moisture Loss
Extended refrigerated transport often leads to freezer burn, surface desiccation, and moisture degradation caused by micro-leaks and fluctuating temperatures. To protect your food quality, each Container Blast Freezer Room for Pre-cooked Food incorporates ≥100mm high-density polyurethane (PU) integral foaming insulation boards with an ultra-low thermal conductivity of ≤0.024 W/(m·K). Paired with double-layer sealed doors, external heat infiltration is effectively blocked to maintain a rock-solid internal environment.

Optimized Airflow Design via CFD Simulation
Pre-cooked meals packaged in diverse boxes, pouches, or stacked combinations easily create uneven density zones that obstruct cold air circulation. We engineer return air paths tailored directly to your specific loading methodology. For non-standard and high-capacity projects, we utilize advanced Computational Fluid Dynamics (CFD) fluid simulations combined with rigorous physical airflow testing to eliminate dead zones and ensure uniform cooling across every pallet.

Technical Specifications & Structural Parameters
| Items | Parameters |
| Container Cold Storage Size | Standard 20ft / 40ft, and Fully Non-Standard Customization |
| Design Operating Temperature | Below -18℃ |
| Temperature Control Accuracy | ±1℃ |
| Insulation Board | ≥100mm High-Density PU Integral Foaming Insulation Board |
| Heat Conductivity Coefficient | ≤0.024 W/(m·K) |
| Container Cold Storage Door | Double Sealing Gasket System |
| Control System | PLC Intelligent Microcomputer Control |
| Defrosting Mechanism | Automatic Defrosting |
| Fault Protection | Automated Fault Self-Diagnosis |
| Remote Control & IoT | Optional IoT Remote Monitoring Module |
| Temperature Recording | Optional Full-Process Real-Time Temperature Logger |
| Internal Customization | Anti-Squeeze Partitions, Buffer Supports, Airflow Baffles |
Intelligent PLC Control and Complete Traceability
Every unit is governed by an advanced PLC intelligent control system capable of automated temperature regulation, active defrosting cycles, and comprehensive fault self-diagnosis. For food exporters and logistics providers requiring strict regulatory compliance, we offer integrated IoT remote monitoring and full-process temperature recorders, enabling real-time data tracking, cloud uploading, and complete cold chain traceability.

Rigorous Manufacturing, Testing, and Quality Assurance
To guarantee absolute reliability in the field, each unit undergoes an uncompromising 72-hour continuous ex-factory operation test simulating maximum thermal loads and severe ambient temperature differentials. We verify every critical metric, including continuous refrigeration performance, precision thermostat response, container airtightness, watertight integrity, and internal airflow distribution verified against prior CFD models.

Versatile Logistical Applications
Designed for seamless integration across the entire frozen food supply chain, our systems excel in multiple operational environments:
- Prepared Food Factory Direct Delivery: Move products straight from production line rapid freezers into the container cold storage for continuous, uninterrupted cold-chain transit to regional distribution hubs.
- Ports and Logistics Transshipment: Serve as high-performance temporary refrigeration nodes to supplement warehouse capacity during seasonal volume surges or port bottlenecks.
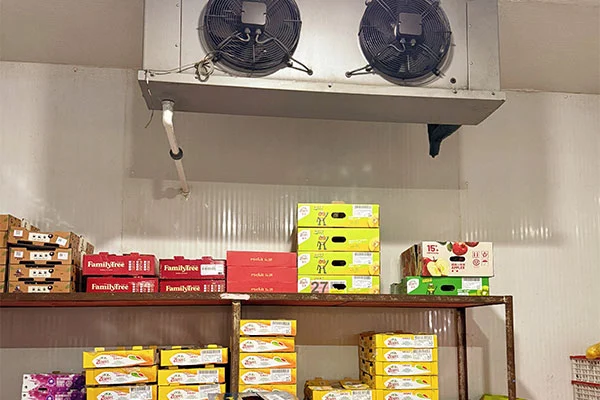
- Food and Fresh Produce Distribution: Act as mobile, climate-controlled cold storage and distribution links for restaurant chains, catering networks, and wholesale food distributors.

Customized Engineering Services
We recognize that no two food processing operations are identical. Beyond standard 20ft and 40ft footprints, we deliver fully customized engineering solutions tailored to your exact product types, packaging geometries, loading techniques, and environmental requirements. From bespoke anti-squeezing partitions and structural buffer supports to specialized door seals and IoT packages, we build the exact system your logistics operation demands.

Comprehensive Global Service and Technical Support
Purchasing our equipment is the beginning of a long-term partnership. We provide end-to-end support encompassing project design, precision manufacturing, installation guidance, commissioning, and lifelong technical assistance. Every delivery includes detailed operating manuals and troubleshooting documentation. In the event of technical challenges, our global network of authorized service partners—backed by our direct engineering team—provides rapid remote diagnostics and debugging support.

Certificates & Quality Standards:


Frequently Asked Questions (FAQ)
Can this device directly freeze room-temperature pre-prepared food down to -18℃?
No. This system is engineered specifically for the stable storage and transport of pre-prepared foods that have already undergone rapid freezing. If you require initial room-temperature rapid freezing capabilities at your facility, please consult our engineering team for a dedicated blast freezing system configuration.
Can you manufacture non-standard sizes larger than standard 20ft and 40ft containers?
Yes. We specialize in custom spatial engineering and can design and fabricate non-standard container dimensions to match your site constraints, payload volumes, and specific transportation requirements.
How does the unit prevent odor cross-contamination between different pre-prepared dishes?
Our containers utilize airtight hermetic sealing, independent zoning structures, and customizable internal partitions tailored to your product packaging. However, for shipments involving exceptionally pungent raw ingredients, we still recommend utilizing distinct barrier packaging or separate transit runs.
Is complete temperature tracking available throughout the entire transit process?
Yes. You can optionally equip your unit with a full-process digital temperature recorder and an IoT remote monitoring suite, allowing you to access real-time status updates and historical audit logs.
Secure Your Cold Chain Solution Today
Whether you require a reliable Container Blast Freezer Room for Pre-cooked Food for sea freight, overland distribution, or port transshipment, our engineering team is ready to design a robust, energy-efficient system matched perfectly to your cargo packaging and target thermal profile. Contact our experts today to discuss your project specifications.

Send Inquiry
Contact Info
-
Address
Xinyuan Avenue, Sangzidian Subdistrict, Tianqiao Borough, Jinan City, Shandong Province, China
-
Tel
-
Submit your project specifications to receive tailored guidance, technical drawings, and cheap factory-direct wholesale pricing from our engineering team today.
Related Products


News Recommendations